Scheduled maintenance is built on averages. Change the oil at the stated hours, do the top end at the stated interval, and a fleet of engines running typical duty cycles will mostly behave. It is a reasonable default and it is how most mining sites run.
The problem is that a gas engine driving a continuous mining load is not running a typical duty cycle. It runs near full load, continuously, often on field gas of variable quality, frequently in a climate that is harder than the design case. Averages built elsewhere do not describe it well, and the engine that fails between scheduled services is the one that costs you.
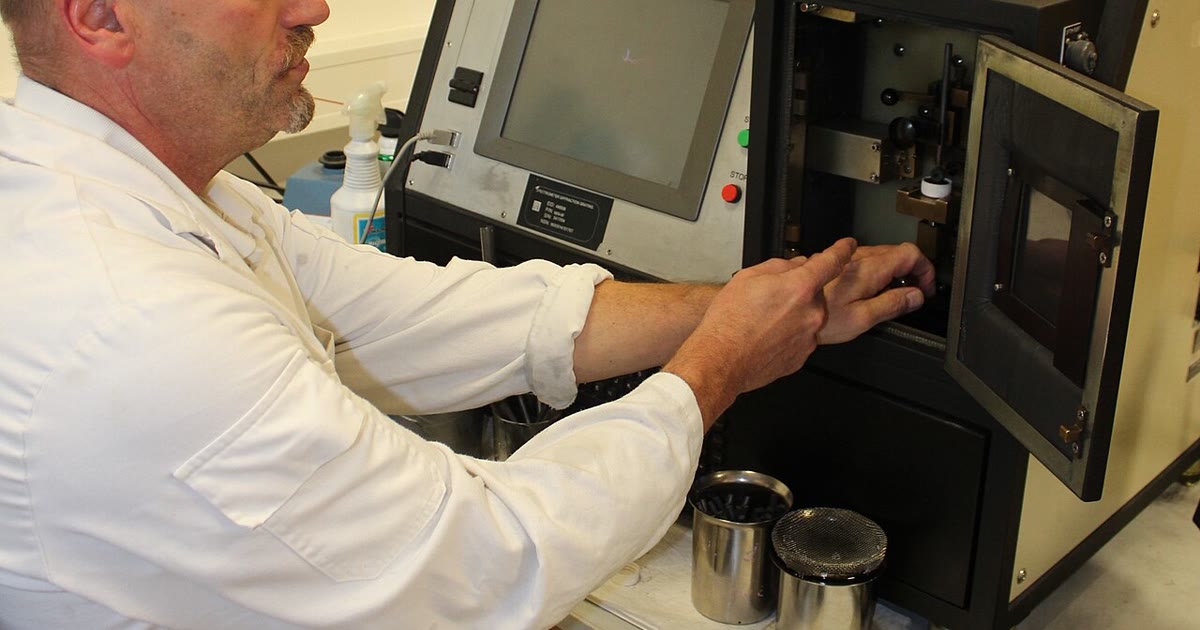
Oil analysis closes that gap. It is condition-based rather than calendar-based, it is inexpensive, and it is the single most informative diagnostic available on a reciprocating engine short of opening it up. This guide covers how to use it alongside the interval schedule set out in our guide to gas engine maintenance intervals and overhauls.
What a sample actually tells you
A standard analysis returns three families of information, and the value is in reading them together rather than one at a time.
Wear metals
Parts per million of the metals the engine is made of, which tell you which component is wearing and roughly how fast.
- Iron points at liners, rings, camshaft and valve train.
- Copper and lead point at bearings. Lead in particular is worth attention because it often moves first.
- Aluminium points at pistons.
- Chromium points at rings, where they are chrome-faced.
- Silicon is usually not wear at all, it is dirt, and it means your air filtration is admitting abrasive. Rising silicon alongside rising iron is a filtration problem presenting as an engine problem.
The number on its own is close to meaningless. What matters is the trend, normalised for hours on the oil. A single elevated reading is a prompt to resample. Three samples climbing is a finding.
Fluid properties
Viscosity tells you whether the oil still is what it was. Rising viscosity usually means oxidation and the oil is getting tired. Falling viscosity means something is diluting it, which on a gas engine usually means fuel.
Total base number measures the oil’s remaining capacity to neutralise acids, and it falls over the oil’s life. When it approaches the condemning limit the oil is no longer protecting the engine regardless of how clean it looks.
Oxidation and nitration both rise with hours and heat, and nitration in particular is a gas-engine concern because of how these engines burn.
Contamination
Coolant in the oil is the finding nobody wants and everybody should look for. Glycol in a sample means a head gasket, a liner seal or a cracked component, and it is urgent because glycol attacks bearings quickly. A rising sodium or potassium reading can be the earliest sign before visible glycol appears.
Water is a separate concern and is common where an engine runs cool or sees heavy condensation cycling. Fuel dilution shows up as falling viscosity and points at combustion or fuelling problems upstream.
Why gas engines on mining load need this more
Three things make a mining genset a harder case than the same engine in standby service.
The load never varies. A standby set runs occasionally. A mining set runs at high load continuously, which means sustained thermal loading and no cool periods in which the oil recovers.
Fuel quality is variable. Field gas is not pipeline gas. H2S, heavier liquids and changing BTU all change combustion and therefore what ends up in the oil. If the gas conditioning upstream is marginal, the oil will show it before anything else does. Our guide to gas quality conditioning covers that side.
Site conditions are harsh. Dust is the one that matters most, because it arrives as silicon and leaves as iron. Our guide to air filtration and dust management covers the fleet side, and the same ambient conditions reach the engine air intake.
Building a programme that works
The programme is simple and most of its value comes from consistency rather than sophistication.
- Sample at a fixed interval, expressed in engine hours rather than calendar time, and sample every unit rather than the one you are worried about. The comparison between units on the same site is one of the most useful signals available.
- Sample the same way every time. Same port, same method, with the engine at operating temperature. A sample drawn from a cold sump after a weekend tells you about the sump, not the engine.
- Label properly. Unit identifier, engine hours, hours on the oil, and whether anything was added. A sample without hours on the oil cannot be normalised and is largely wasted.
- Use one laboratory. Methods and limits vary between labs, and switching mid-programme breaks your trend line at exactly the moment you want to rely on it.
- Act on the trend, not the flag. Laboratory alarm limits are generic. Your own baseline for your own engines on your own gas is more informative after a few samples than any generic limit.
Reading two samples side by side
An example makes the method concrete. Two units on the same pad, same engine model, same gas, both at roughly the same hours on the oil.
Unit A returns iron climbing steadily across three samples, silicon climbing alongside it, everything else stable. That pattern is not an engine problem in the sense of a component failing. It is abrasive ingestion, and the fix is at the air intake. Overhauling that engine would consume a great deal of money and the iron would start climbing again within weeks.
Unit B returns iron flat, silicon flat, but lead moving up across two samples with a small rise in copper. That is a bearing signal, and it is the one that justifies intervening ahead of the scheduled interval, because a bearing that fails in service takes far more of the engine with it than a bearing replaced on a planned shutdown.
Same laboratory, same cost, two completely different actions. Neither would have been visible from the hour meter, and an interval-based schedule would have treated both engines identically.
What this does not catch
Oil analysis is diagnostic, not comprehensive, and it is worth being clear about its limits so it is not relied on for things it cannot see.
It will not tell you about anything outside the lubricated path. Turbocharger damage may show up late or not at all. Ignition faults, valve timing and control problems do not appear in an oil sample. Nor will it warn you about an imminent failure that happens quickly rather than progressively, because a programme sampling every few hundred hours only sees what develops between samples.
It also says nothing about the rest of the container. Electrical terminations, cooling system fouling and the mining hardware itself all need their own monitoring, and the controls layer that watches them is covered in our guide to SCADA and PLC controls.
What to do when a sample comes back bad
Resist the instinct to immediately change the oil. Changing the oil removes the evidence, and a fresh sample on fresh oil tells you nothing about the trend you were trying to read.
The useful sequence is to resample to confirm, correlate against what the engine is actually doing on temperatures, pressures and load, and only then decide. A confirmed glycol finding is a shutdown. A confirmed and climbing bearing metal is a planned intervention before the scheduled overhaul. Rising silicon is a filtration fix, not an engine fix.
Record the decision and the outcome. The value of a condition-monitoring programme compounds, and it only compounds if someone can look back and see what the samples predicted and what actually happened.
Where it fits
Oil analysis does not replace the interval schedule, it informs it. It tells you which engine needs attention sooner than the calendar suggests and, equally usefully, which one does not and can safely run to interval. On a fleet that is the difference between a maintenance budget spent evenly and one spent where it matters. It also feeds directly into what you hold on the shelf, covered in our guide to spare parts inventory strategy.
Rax Mining operates containerized natural gas mining units where the engine is the asset that determines uptime, and condition monitoring is part of how a site is run rather than an optional extra. If you are planning a deployment and want the maintenance and monitoring programme defined up front, our consulting team can work through it.
Explore Rax Mining
- Bitcoin Miner Hosting — Competitive rates from $0.075/kWh
- NatGas MDU Units — 1MW modular datacenter containers
- Mining Profitability Calculator — Estimate your mining returns
- Our Facility — Tour our mining infrastructure