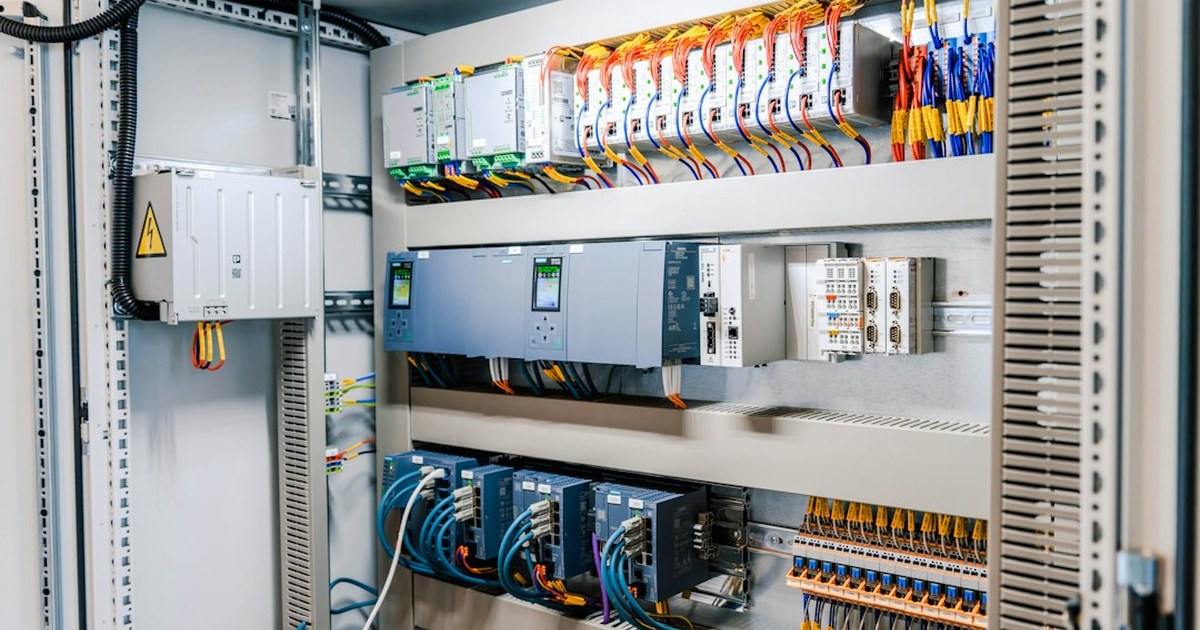
Electrical gear at a mining site gets an enormous amount of attention for about six months. It is sized, specified, quoted, argued over, delivered late, and energized. Our guides to electrical infrastructure and transformer and switchgear lead times cover that phase in detail, because it is where the money and the schedule risk sit.
Then it works, and nobody looks at it again.
That is the problem. Switchgear is not a passive object. It contains moving mechanisms, current-carrying joints that loosen, insulation that accumulates contamination, and protective devices with settings that were correct for a site that has since changed. None of that announces itself. The first symptom of neglected gear is usually the event it was supposed to prevent.
Why mining sites are harder on gear than most industrial loads
A mining load is unusual in ways that matter to switchgear specifically.
It runs near full rating continuously. Most industrial facilities have a duty cycle; a mining hall largely does not. Joints that would see a few hours a day at full current see it around the clock, and heat cycling at connections is what drives them loose over time.
The environment is also dirtier than a typical electrical room. Air-cooled halls move enormous volumes of outside air, and whatever is in that air gets distributed. Dust on insulating surfaces is a tracking path; dust in a mechanism is friction.
And the load changes. Sites curtail, add containers, swap miner models with different power profiles, and rebalance phases. Our guide to load balancing and phase management covers the operational side of that. The electrical consequence is that the assumptions behind the original protection settings quietly stop being true.
What a maintenance program actually consists of
There is an established standard for this. NFPA 70B covers electrical equipment maintenance and sets out condition-based intervals by equipment type and operating environment. It is the document to work from rather than inventing a schedule, and it is worth reading in its current edition because the guidance has been revised.
In practice the program comes down to five activities.
Infrared scanning under load
This is the single highest-value check and the easiest to arrange, because it is non-invasive. A thermographic survey taken while the site is running shows connections that are running hotter than their neighbors, which is the signature of a loose or corroded joint long before it fails.
The critical detail is that it must be done under meaningful load. A scan taken during a curtailment shows nothing, because the heat that reveals the defect is not being produced. That constraint is specific to sites that curtail regularly, and it means the survey has to be scheduled around operations rather than around the contractor’s convenience.
Our guide to predictive maintenance covers thermal imaging as a general technique across the site. The switchgear-specific point is that findings need a defined response: a threshold above ambient at which a joint gets scheduled for correction, and a higher one at which it gets corrected now.
Connection torque
Bolted connections carry current through a clamped interface, and the clamping force is what makes it a low-resistance joint. Thermal cycling relaxes that force. A loose joint heats, and heat accelerates the loosening, which is why these failures escalate rather than sitting stable.
Checking torque means a planned outage, because it is physical work on de-energized equipment. Values are specified by the manufacturer for the specific hardware and must come from that documentation, not from a general table.
Cleaning and inspection of insulating surfaces
Contamination on insulation creates a path for current to track across a surface that was designed to block it. In a dusty hall this accumulates faster than most operators expect, and the intake side of an air-cooled building is the worst case, because the room is effectively downstream of whatever the site sits in. Agricultural dust, road dust off an unpaved access route, and salt in coastal air all behave differently and none of them are harmless.
Inspection also catches the things that are only visible when a panel is open: moisture ingress and the staining that shows where water has been, corrosion on bus supports, heat discoloration at terminations that an infrared survey may have missed because the joint was not loaded at the time, and evidence of rodent activity, which is a real and underrated hazard in remote buildings and a plausible cause of a fault that will otherwise never be explained.
Mechanism exercise and breaker testing
A circuit breaker that has sat closed for years may not open correctly when it is finally asked to. The mechanism is mechanical, and mechanical things that never move seize. Exercising breakers on a schedule keeps them functional.
Beyond exercising, electronic trip units can be tested with secondary injection to confirm they actually trip at their programmed settings. This matters because the settings are an assumption until verified, and a breaker that does not trip as designed invalidates the fault analysis the whole system rests on.
Reviewing the protection settings against the site as it is now
This is the step that gets skipped, and on a growing mining site it is the one most likely to be wrong.
Protective device settings come out of a coordination study based on the site’s fault current and load at the time of the study. Our guide to short circuit studies explains how that analysis works. The settings are correct for that snapshot.
Sites then change. Capacity gets added, a transformer gets upgraded, the utility reconfigures its side, more generation gets installed. Each of those alters available fault current, and the settings that were correct are now approximations. Re-running the study after a material change, and updating settings to match, is what keeps protection coordinated rather than nominally present.
Arc flash is the reason the paperwork matters
Everything above is also a safety program, because the hazard that maintenance work exposes people to is arc flash.
Arc-flash incident energy depends on available fault current and on how long the protective device takes to clear the fault. Both are things the maintenance program governs: the fault current comes from the study, and the clearing time depends on a breaker that trips as designed. A breaker that trips slowly because its mechanism is neglected raises incident energy above what the labels on the equipment claim, which means the protective equipment people are wearing was selected against a number that is no longer true.
Our guide to arc-flash boundary calculations covers the analysis and the protective equipment requirements. The maintenance connection is the part that gets missed: the labels are only as accurate as the condition of the gear behind them.
Racking is the highest-risk routine task
Inserting or withdrawing a drawout breaker from its cubicle puts a person directly in front of energized equipment while a mechanism does something mechanical. It is the task most associated with serious incidents, and it is routine enough that familiarity erodes caution.
The mitigations are well established and worth insisting on: de-energize where the work allows it, use remote racking equipment so the operator stands outside the arc-flash boundary where it does not, and treat the manufacturer’s procedure for that specific gear as the procedure rather than relying on what somebody did at a previous site.
Getting it scheduled on a site that never wants to stop
The honest obstacle is not cost. It is that the work needs the gear de-energized, and a mining site stopping is immediately visible as lost revenue, which our guide to downtime costs quantifies. There is always a reason to defer.
Three things make it happen in practice. Schedule it against a curtailment window, when the site is already down and the revenue is already forgone; on sites that curtail regularly this converts the single largest objection into a non-issue. Sequence the work so one section is isolated at a time rather than the whole site, which turns a full outage into a series of partial ones. And decide the interval in advance, in writing, so that deferring becomes a decision somebody has to make rather than the default that happens when nobody raises it.
The gear that fails is almost never the gear somebody was worried about. It is the section nobody has opened since commissioning, because that is where a loose connection has had the most time to get worse.
The practical version
For a site in operation: get a thermographic survey done under real load and establish what happens when it finds something; obtain the manufacturer’s maintenance documentation for the specific gear installed; find out whether the protection settings have been reviewed since the last capacity change; and confirm whether anyone has ever tested a trip unit rather than assuming it works.
For a site in design: specify remote racking capability, insist on receiving maintenance documentation as a deliverable rather than chasing it later, and put the first maintenance interval into the operating budget before the site energizes.
None of this generates revenue, which is why it loses every argument against something that does. It is worth remembering that the failures it prevents take out the whole site, not one container, and that they tend to happen to equipment everyone had stopped thinking about.
Operators who would rather not run an electrical maintenance program can place machines in a facility that already does. Our breakdown of what hosting costs per kilowatt-hour covers what that includes, and you are welcome to talk to our team about either path.
Explore Rax Mining
- Bitcoin Miner Hosting — Competitive rates from $0.075/kWh
- NatGas MDU Units — 1MW modular datacenter containers
- Mining Profitability Calculator — Estimate your mining returns
- Our Facility — Tour our mining infrastructure